

Global Supplier of Sustainable Blended Fabrics
We work with leading fashion brands and designers, offering in-stock fabrics, flexible low-MOQ programs, and fast response for efficient development and production.

Traceable & Responsible Knit Fabric Solutions at Flexible MOQ
✦ Traceable raw materials with responsible sourcing
✦ In-stock and low-MOQ support for agile development
✦ Testing-ready fabrics with quality inspection and compliance support
Explore Our Core Fabric Series
Regen-tech Fashion’s fabric range covers a broad selection of natural fibers and commonly used blended constructions, including Lenzing™ Lyocell, Merino wool, linen, cotton, and functional or recycled fiber blends. Designed to support diverse design and development needs, our fabrics are suitable for a wide range of applications.
Fabrics are available from stock or flexible low-quantity programs, and can be used for dyeing, printing, and related testing requirements, supporting efficient development and stable supply.


Start Your Next Collection with Us
What Is Scuba Knit Fabric?
What Is Scuba Knit Fabric?
Scuba knit is a structured, double-knit fabric known for its smooth surface, consistent body, and moderate two-way stretch. Compared with lightweight single-jersey fabrics, scuba is typically denser—often ranging from 280 to 380 gsm—and has a tightly knitted structure that gives it a fuller, more substantial feel. It’s most commonly made from polyester or polyester-spandex blends (e.g., 92% polyester / 8% spandex), while recycled polyester versions are also available.
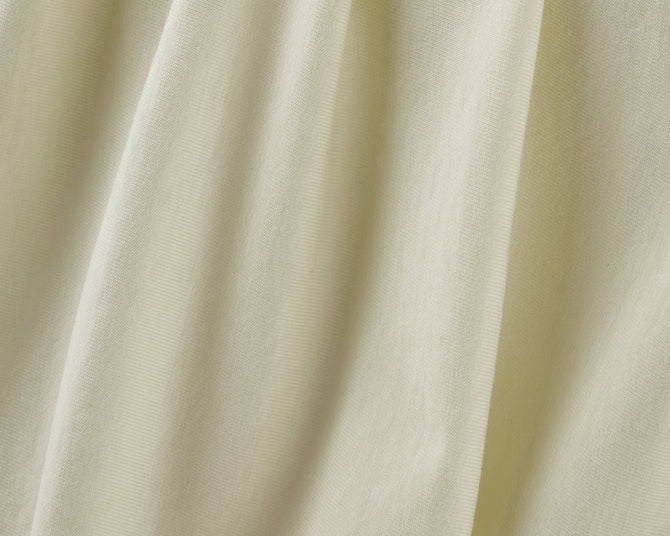
Visually, scuba knit has a clean, almost leather-like finish—sleek and uniform, with minimal texture or sheen depending on finishing. Its hand feel is firm yet supple: not stiff, but distinctly substantial, offering reassuring resistance when stretched and snapping back reliably. This combination of stability and recovery makes it especially valuable in contemporary apparel where silhouette integrity matters as much as comfort.
Key Characteristics That Define Its Performance
- Structure & Recovery: Scuba’s double-knit architecture gives it inherent shape retention—ideal for garments that must hold clean lines without sagging or bagging over time.
- Stretch & Fit: With balanced horizontal and vertical stretch (typically 20–30% in each direction), it supports precision-fit patterns while accommodating movement—critical for body-conscious styles.
- Drape & Body: It drapes with controlled fluidity—not stiff like coated fabrics, nor soft and cascading like rayon jersey. Instead, it falls in smooth, defined folds, supporting architectural silhouettes such as cocoon coats, sculptural skirts, or tailored sweatshirts.
- Surface & Finish: The fabric’s smooth face resists pilling and holds prints and solid dyes evenly. Its low nap and tight loop formation also contribute to durability during repeated wear and laundering.
Apparel Applications: Where Structure Meets Design Intent
Scuba knit excels where garment design prioritizes form, function, and refined ease. Its physical properties align directly with specific apparel categories:
- Tailored Casualwear: Think modern sweatshirts, zip-front hoodies, or elevated joggers—pieces that balance sporty comfort with polished proportions. Scuba’s body prevents ballooning at the hem or sleeves, keeping seams sharp and volumes intentional.
- Contemporary Dresses & Skirts: A-line, pencil, or asymmetrical midi skirts rely on scuba’s ability to hold shape while moving with the wearer. Unlike stiffer wovens, it offers silent flexibility; unlike fluid knits, it avoids cling or distortion at the hip or thigh.
- Lightweight Outer Layers: Structured blazers, cropped jackets, and vest shells benefit from scuba’s drape control and clean interior—no lining needed in many cases. Its moderate weight bridges the gap between traditional suiting and everyday layering fabrics.
- Body-Conscious Tops & Bodysuits: For ribbed or seamless-style tops requiring support without compression, scuba delivers gentle shaping and seam resilience—especially important in cut-and-sew production where seam roll or torque can compromise fit consistency.
Sustainability and B2B Considerations
From a sourcing perspective, scuba knit is gaining traction among forward-thinking apparel brands committed to responsible material innovation. Recycled polyester-based scuba reduces reliance on virgin feedstocks and maintains identical performance—making it a drop-in sustainable alternative for existing patterns. For product development teams, scuba’s consistency across dye lots and reliable behavior in cutting, sewing, and finishing simplifies sampling and scale-up—reducing waste and rework in early-stage prototyping.
Why Scuba Knit Endures in Modern Collections
Scuba knit is more than a trend-driven textile—it’s a functional response to evolving design priorities: clean aesthetics, intentional volume, and lasting wearability. Its unique balance of structure and stretch enables designers to explore silhouette with confidence, while its adaptability to recycled and blended compositions supports long-term sustainability goals. For apparel brands building versatile, seasonless collections, scuba knit remains a foundational material—not because it’s flashy, but because it performs consistently, wears well, and translates design vision into dependable garment reality.
FAQ
What is scuba knit fabric, and how does it differ from other knits like jersey or interlock?
Scuba knit is a dense, double-knit fabric with a smooth, uniform surface and moderate two-way stretch (20–30% in both directions). Unlike lightweight jersey or fluid interlock, scuba typically weighs 280–380 gsm and features tightly locked loops on both sides—giving it superior structure, shape retention, and recovery. Its firm yet supple hand feel and controlled drape make it ideal for precision-fit, architectural garments where silhouette integrity is critical.
What fiber compositions are most common—and increasingly sustainable—in scuba knit for B2B sourcing?
Standard scuba knit is commonly made from polyester-spandex blends (e.g., 92% polyester / 8% spandex) for optimal stretch and recovery. However, many forward-thinking B2B suppliers now offer eco-conscious alternatives—including versions with 100% recycled polyester (rPET) or blended with TENCEL™ lyocell—to improve breathability and sustainability while maintaining the fabric’s signature structure and performance.
Why is scuba knit especially well-suited for tailored casualwear and structured outer layers?
Scuba’s dense double-knit construction provides inherent body and minimal distortion, preventing ballooning at hems or sleeves—key for elevated joggers, zip-front hoodies, and cropped jackets. Its clean interior often eliminates the need for lining, and its controlled drape supports sharp seams and intentional volumes without sacrificing comfort or movement—bridging the gap between sportswear ease and tailoring precision.
How does scuba knit perform in terms of durability, pilling resistance, and print/dye consistency?
Thanks to its tight loop formation, low nap, and smooth face, scuba knit resists pilling and holds solid dyes and digital prints evenly across the surface. Its density and polyester content contribute to long-term durability through repeated wear and laundering—making it a reliable choice for high-turnover collections and performance-driven fashion brands seeking consistent quality and color fidelity.
Can scuba knit be used for body-conscious dresses and skirts—and how does it compare to traditional wovens or fluid knits?
Yes—scuba knit excels in A-line, pencil, and asymmetrical midi skirts and dresses. It offers silent flexibility (unlike rigid wovens) while avoiding cling or hip distortion (unlike fluid rayon or cotton jerseys). Its balanced stretch and strong recovery ensure the garment maintains clean lines during movement, delivering refined ease and lasting shape retention—ideal for contemporary, body-aware silhouettes.
Global Fabric Sourcing & Supply Network
Regen-tech Fashion is a differentiated knit fabric supplier and manufacturer serving fashion brands, designers, and apparel partners worldwide. Our fabric portfolio covers natural and blended fiber options—including Lenzing™ Lyocell, Merino wool, linen, cotton, and commonly used blends such as viscose, polyester, nylon, modal, and spandex—supporting modern product development with reliable supply and consistent quality.
We offer 4 key programs:
-
Ready Stock (core knit qualities with stable availability and flexible quantities)
-
Low-MOQ Development (sampling and small-batch programs for agile collections)
-
Custom Production (fabric development, finishing options, and structured quality control)
-
Testing & Compliance Support (inspection coordination, test requests, and documentation support)
Explore our fabric series to match your next collection—from everyday essentials to structured knits and active-inspired blends. For inquiries or support, contact our team for fabric recommendations, availability, and order guidance.
Related Blogs
Add a short description for your brand news

Nylon vs Polyester for Stretch Knit Fabrics: Which Performs Better in Modern Knitwear?

Knit Structures Used in Athleisure Fabrics: A Guide for Performance & Fabric Development

What Is Scuba Fabric Made Of? Polyester, Spandex & Beyond